Pusher Furnace Within the Industry: Key Applications and Advancements
2026-10-04
Ask any production engineer about the unseen engine of continuous heat treatment, and pusher furnaces often top the list—yet their story is rarely told. From precision sintering in electronics to stress-relieving aerospace alloys, these furnaces are quietly reshaping what's possible. Join us as we unpack the key applications and breakthrough advancements that matter right now, with insights aligned to THINKING-LONG's forward-driven approach.
What Makes a Pusher Furnace the Default for High-Volume Sintering
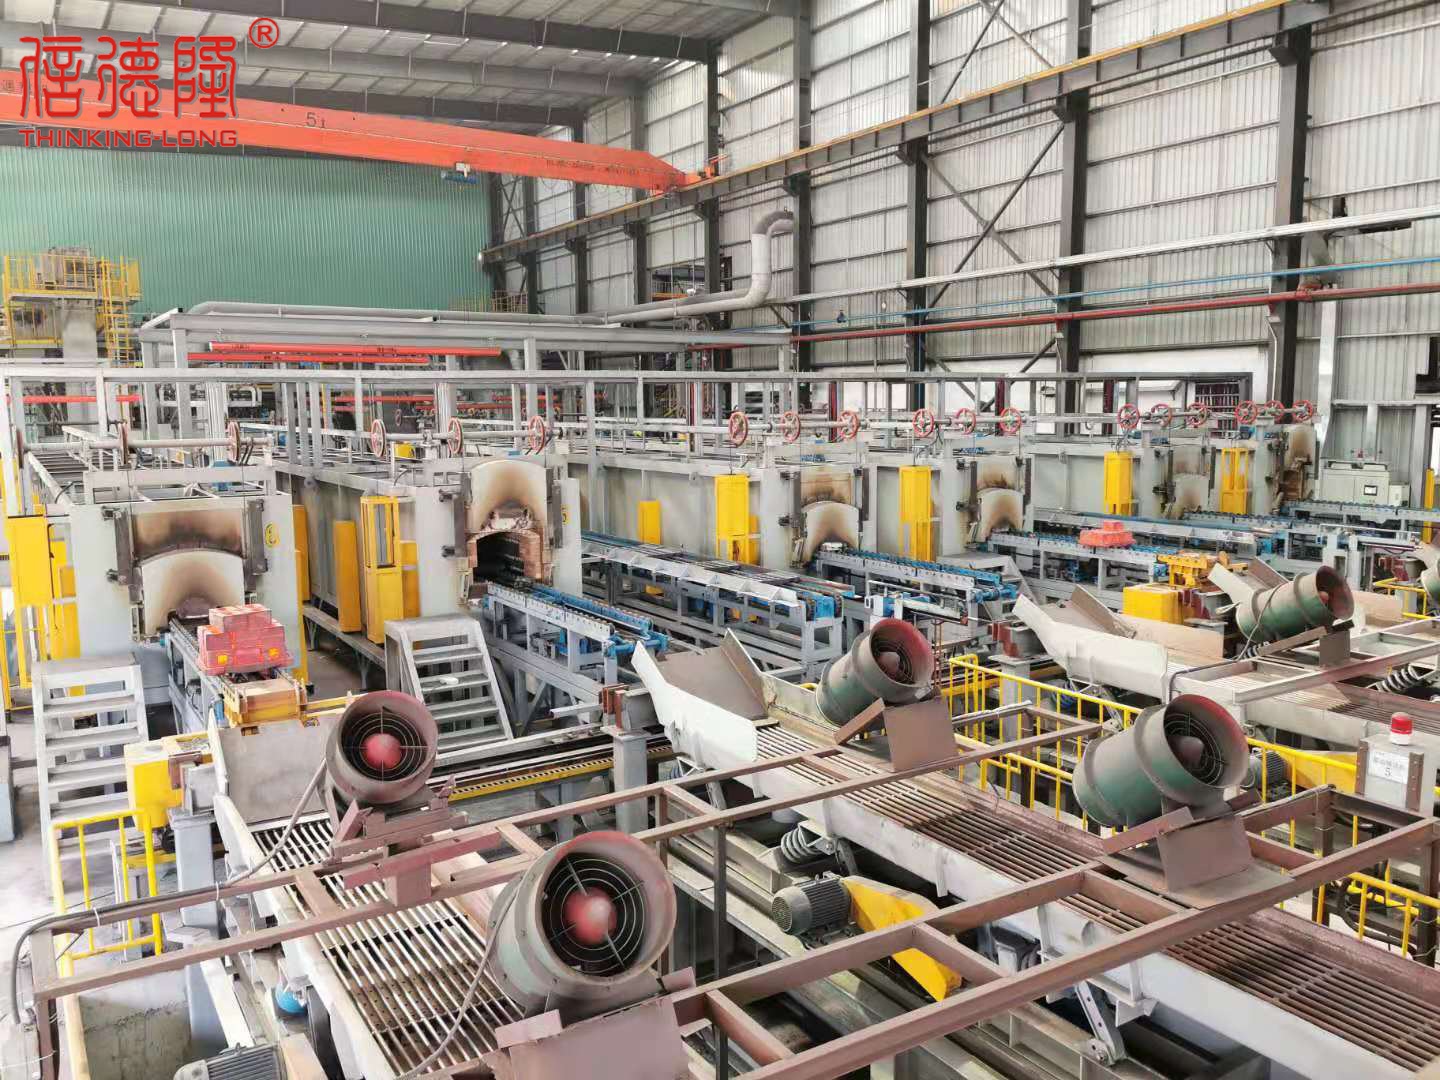
In high-volume powder metallurgy, the pusher furnace earns its place not through a single breakthrough feature but through a rhythm that batch equipment cannot match. Parts move through preheat, sintering, and cooling zones on a fixed cadence, so every tray sees the same thermal profile hour after hour. This repeatability removes the temperature drift and load-dependent variability that often plague box furnaces, making the pusher design especially attractive when a line is expected to run the same alloy mix for weeks at a time.
The real lever is how the furnace decouples output from operator attention. Multi-row loading and continuous infeed mean throughput climbs without adding shifts or manual handling between cycles. Combined with separate atmosphere curtains at each zone boundary, the system holds carbon potential and dew point steady while doors stay closed, which cuts both oxidation risk and post-sinter rework.
Energy per kilogram also tends to drop as the furnace reaches its designed throughput. Instead of repeatedly heating and cooling a chamber, the pusher furnace maintains a stable thermal gradient and lets product move through it. For high-volume sintering, that steady-state operation translates into predictable delivery dates, tighter dimensional control, and fewer surprises when scaling from pilot runs to full production.
Keeping Parts Moving Without Breaking the Atmosphere Seal
Moving parts through a sealed chamber wall typically means dealing with rods, shafts, or carriages that have to slide or spin without letting the controlled atmosphere leak out. Welded metal bellows and edge-welded diaphragms work well for linear motion because they flex instead of slide, eliminating the usual wear path where outside air could find its way in. For rotary feedthroughs, magnetic couplings take this idea further: torque passes through a non-magnetic barrier, so the shaft inside never physically touches the drive outside.
Continuous rotation under vacuum or inert gas often relies on ferrofluidic seals, where a ring of magnetic fluid stays trapped in the narrow gap around the shaft. That film can hold a pressure differential while the shaft turns at high speed, though it does have a finite leak rate and needs periodic replacement. The right combination depends on stroke length, rotational speed, and how sensitive the process is to trace contamination, but splitting the motion between bellows and magnetic or ferrofluid stages keeps the seal intact without slowing down the operation.
When Continuous Push Outperforms Batch for Delicate Components
For parts that flex, fracture, or deform under sudden force, a steady, uninterrupted feed changes everything. Batch methods often rely on discrete movements—start, stop, reposition—each one introducing impact and vibration. Continuous push eliminates those micro-collisions by keeping the component in motion along a controlled path. The result is fewer hairline cracks, less surface marring, and a dramatic drop in scrap rates for thin-walled housings, ceramic inserts, and precision-molded electronics.
Temperature also plays a quiet but decisive role. In batch processing, dwell time between stations lets heat soak unevenly into fragile substrates, warping them before the next cycle even begins. A continuous push spreads thermal exposure evenly across the entire travel length, so no single spot overheats or cools too quickly. This becomes critical with glass-reinforced polymers and laminated films, where a two-second pause can mean the difference between a clean edge and a curled, unusable lip.
Then there's the matter of alignment. Delicate components rarely forgive even half a millimeter of drift. Batch transfers rely on pick-and-place accuracy that degrades with speed, but a continuous push keeps the part constrained by guide rails or vacuum belts from entry to exit. That constant contact removes the opportunity for bounce, skew, or double-feeding. In practice, lines running continuous push on connector pins and micro-optical lenses see first-pass yield climb into the high nineties—not because the operators got better, but because the process stopped handing fragility a chance to fail.
The Latest Insulation and Burner Upgrades Worth Noticing
Refractory and insulation choices have shifted noticeably over the last year. Microporous boards and aerogel blankets are replacing traditional ceramic fibre in furnace linings, mostly because they deliver the same thermal resistance at half the thickness. That extra space lets operators increase load capacity or simply reduce surface temperatures on existing shells. Installation is less dusty than older fibre work, which maintenance teams appreciate.
On the burner side, the quiet rollout of staged combustion and flue gas recirculation has pushed NOx levels down to single-digit ppm without resorting to expensive SCR systems. New burner controls now tie oxygen trim sensors directly to fuel valves, so air-to-fuel ratios adjust on the fly instead of waiting for a scheduled tune-up. The result is steadier flame geometry and fewer hot spots inside the chamber.
Pairing these upgrades creates a compounding effect. A furnace retrofitted with low-thermal-mass insulation and a modulating low-NOx burner typically reaches setpoint faster and retains heat between cycles. Shops running batch heat treatment have reported noticeably lower gas bills and tighter temperature uniformity after replacing just the lining and burner block.
Where Pushing Fits for Powder Metal and Technical Ceramics
In powder metal and technical ceramic production, pusher furnaces earn their keep when part geometries and process demands line up with continuous linear handling. Components that can be loaded onto flat setters or saggers and moved through a hot zone without shifting or sticking are prime candidates. This includes smaller pressed compacts, injection-molded ceramic bodies, and debound parts that need a steady, repeatable thermal profile rather than batch-style variability.
The technique also fits well where high throughput matters more than extreme flexibility. A pusher system can maintain tight push rate, giving every piece roughly the same residence time at temperature. That uniformity is valuable for sintering ferrites, alumina, zirconia, and PM steels where density, grain size, and dimensional tolerance respond to small changes in peak temperature or cooling rate.
However, pushing is not a blanket solution. It works best for parts that can tolerate gentle contact with adjacent trays or boats and do not require individual atmosphere control. Complex shapes with delicate overhangs, very large cross sections, or materials that outgas heavily may be better served by walking-beam, roller hearth, or batch furnaces. Matching the part’s geometry, production volume, and thermal sensitivity to the pusher’s continuous motion is what separates a reliable process from a bottleneck.
Avoiding the Usual Push-Related Jams and Temperature Drift
Most push-related jams trace back to a simple mismatch between filament diameter, nozzle size, and feed rate. Rather than cranking up the extruder tension, check whether the melt zone is actually keeping pace with the commanded speed. A slightly longer heat break or a more consistent cooling fan curve often eliminates the back-pressure spike that causes the extruder teeth to slip and grind.
Temperature drift is rarely just a bad thermistor. It usually shows up when the heater cartridge cycles too aggressively or when the part cooling fan blows across the block. Lagging the PID values or adding a silicone sock buys enough thermal inertia to flatten the swings. If the drift returns after a few hours, look for a partially seated nozzle or a worn PTFE liner that changes how heat travels up the filament path.
FAQ
The design gives them an almost metronome-like part progression through preheat, boost, diffuse, and quench zones. Since every tray advances by the same fixed increment, case depth uniformity stays tight across thousands of parts, and the mechanical simplicity keeps uptime high even in dusty plant environments.
Instead of relying on a single mixed-gas setting, newer systems use mass flow controllers and oxygen probes that adjust the carbon potential zone by zone. This lets operators hold a narrow window around the oxide reduction boundary without over-carburizing, which was a common problem with older endothermic generators.
One approach is splitting the chamber into independently powered modules that can idle at a lower setpoint when the line pauses. Combined with lightweight ceramic fiber linings and regenerative burners, the furnace can drop from full soak temperature to a standby state and recover within minutes rather than hours.
Large-format tiles need extremely stable support during glaze firing because any slight deflection or roller chatter shows up as surface ripple. A pusher furnace carries the tiles on fixed refractory slabs, so the load path is more static, and the firing curve can be extended without worrying about roller bearing life at high temperature.
Heavy loads can cause skid marks, uneven contact with rails, and occasional jam-ups if the charge expands. Modern hydraulic pushers with force feedback can detect abnormal resistance early and stop or retract before a pile-up occurs. Some plants also use graphite-based rail coatings and optimized tray materials to lower friction and reduce surface defects.
For binder jet metal parts, the green body is fragile and needs a slow, controlled debinding stage before the pores close. A pusher furnace can be configured with a long, low-temperature preheat zone and a staged atmosphere where the binder vapors are extracted before sintering begins. Tray designs with individual part nests also help keep complex geometries from distorting.
The difference usually comes down to thermal expansion management and wear resistance. A good hearth uses interlocking refractory tiles with expansion gaps that prevent buckling, and the side rails are made of a material that resists both oxidation and metal dust buildup. Poor designs often fail within months because the tiles shift and create ledges that catch the pusher plates.
Conclusion
For many production teams, the pusher furnace has quietly become the backbone of high-volume sintering, mainly because its continuous material flow removes the start-stop inefficiencies of batch equipment. The core advantage lies in a carefully engineered atmosphere seal: trays move through heated zones without exposing parts to outside air, which is essential when processing oxidation-sensitive powders or components. Unlike batch furnaces that impose sharp thermal cycles, a well-tuned push system keeps delicate parts moving steadily through preheat, soak, and cooling stages, reducing the internal stress that can crack or distort thin-walled geometries. This steady-state operation also makes it easier to hold tight temperature bands over long runs, a requirement that batch kilns often struggle to meet without costly manual intervention.
Recent insulation and burner upgrades have further strengthened the case for pusher designs. Advanced ceramic fiber linings and low-NOx burners now cut fuel consumption while improving temperature uniformity across the hearth width, which directly benefits powder metal and technical ceramic producers who rely on precise densification curves. In these fields, even a few degrees of drift can alter grain growth or binder burnout rates, so modern pusher systems incorporate zoned heating, automated tray tracking, and pressure-balanced vestibules to avoid jams and thermal lag. Operators have also learned that preventing push-related problems is less about adding sensors and more about matching hearth material, push force, and loading density to the specific product. When those elements align, the pusher furnace offers a balance of throughput, atmosphere control, and process stability that remains hard to replicate with alternative continuous kilns.
Contact Us
Contact Person: Qian Xijun
Email: [email protected]
Tel/WhatsApp: 8613961736750
Website: https://www.thinkinglong.com/