Export AGV Compatible Pallet Supplier Selection Guide for Global Manufacturers
2026-09-16
Most global manufacturers learn the hard way that 'AGV-compatible' is not a universal standard. A few millimeters off in pallet dimensions, and your automated guided vehicle jams, your production line stalls, and your export shipment gets flagged. So how do you separate precision-engineered partners from risky shortcuts? This guide walks through the non-negotiable criteria—from material selection and load ratings to real-world compatibility testing. And when you're ready to move beyond theory, Lanyuda has already solved these challenges for manufacturers across multiple continents.
Where Pallet Precision Becomes the Difference Between Smooth AGV Runs and Line Stops
A pallet that sits even a few millimeters off its expected position can force an AGV to slow, re-align, or abandon the pick altogether. In high-throughput facilities, that hesitation compounds quickly. Operators may blame the vehicle, but the root cause often lives in the pallet itself: warped boards, inconsistent pocket depths, or a load that shifted during transit. Precision here isn't about metrology lab accuracy; it's about repeatability under real floor conditions.
When pallets are built or repaired without strict dimensional control, AGVs spend more time scanning and correcting than moving product. A stop that takes three seconds instead of one might not sound like much, but across a shift with hundreds of transfers, it becomes a line stoppage waiting to happen. The difference shows up most clearly at transfer stands and conveyor handoffs, where the AGV's forks or rollers must meet the pallet exactly the first time.
The practical fix is less about upgrading AGV sensors and more about tightening pallet tolerances where it matters: entry chamfers, bottom board flatness, and consistent runner spacing. Facilities that audit incoming pallets and reject the worst 5 percent often see a measurable drop in unplanned stops without touching the fleet. Precision at the pallet level quietly decides whether the line flows or stutters.
Material Choices That Hold Up When Robots Do the Heavy Lifting
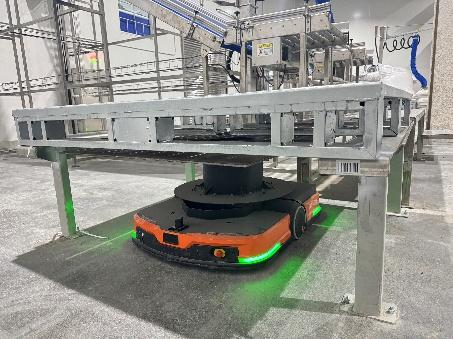
When robots are tasked with heavy lifting, the materials in their structural frames and joints must endure constant stress without permanent deformation. High-strength low-alloy steels like A514 and dual-phase steels provide the necessary yield strength for load-bearing arms, but the push for lighter robots has led to selective use of carbon-fiber-reinforced polymers in non-critical sections. The real challenge is matching material properties to the load spectrum: sustained torque demands high fatigue resistance, while unexpected impacts call for sufficient fracture toughness to avoid catastrophic failure.
Beyond static strength, the internal components that transmit motion face relentless wear. Case-hardened steels such as AISI 8620, after carburizing, offer a hard surface for gears and bearings with a ductile core to absorb shock—a combination that extends service intervals. In parallel, advanced polymer bushings made from PEEK eliminate the need for lubrication in harsh environments, reducing maintenance and preventing contamination, which is especially critical in cleanrooms or food-processing robots.
One often-overlooked factor is thermal stability. Electric motors and gearboxes generate significant heat, which can soften metals and cause dimensional drift. Incorporating aluminum heat sinks with embedded heat pipes or using metal matrix composites like aluminum-silicon carbide helps dissipate heat efficiently, preserving the precise tolerances required for repeatable heavy-duty operations. Selecting materials with high thermal conductivity not only protects the robot's accuracy but also prevents premature failure of nearby electronic components.
What Global Buyers Overlook in Pallet Certification Until a Shipment Gets Flagged
Most buyers assume any pallet with a visible ISPM-15 stamp is automatically compliant. In practice, stamps get forged, reused, or applied to pallets that never underwent proper heat treatment or fumigation. The mark alone tells you almost nothing about the treatment date, the facility that performed it, or whether repairs after treatment introduced untreated wood. A shipment flagged at a foreign port often traces back to a pallet that looked fine in the warehouse but lacked a verifiable trail.
Another blind spot is country-specific nuance. ISPM-15 sets a baseline, but some importing nations enforce stricter bark tolerances, demand additional documentation, or reject pallets with older treatment marks that fall outside accepted validity windows. Buyers who rely on a single compliance checklist for every destination tend to learn this only after customs holds the container. The cost of storage, inspection, and re-export quickly dwarfs any savings from using cheaper unverified pallets.
There is also the quiet problem of mixed loads. A supplier may ship certified pallets for most of an order and slip in a few uncertified units when inventory runs short. By the time the container is opened abroad, the entire shipment can be flagged because one pallet lacks proper treatment. Spot-checking at the loading dock, matching stamps to lot numbers, and keeping photos of each pallet before sealing the container are simple habits that prevent expensive surprises.
Custom Pallet Specs Without the Usual Lead-Time Nightmares
Custom pallets often mean waiting weeks—or months—while suppliers juggle tooling, approvals, and production slots. That delay doesn't have to be the norm. By working directly with a manufacturer that keeps standard components on hand and uses modular design principles, you can get a pallet built to your exact dimensions, load capacity, and material specs without the drawn-out wait. The key is avoiding over-customization where it doesn't add value and instead focusing on adjustable templates that still feel made-to-order.
The usual nightmare starts with a simple request: "We need a pallet that's 48 by 42 inches, but with reinforced corners and a different board thickness." Before you know it, you're stuck in a loop of CAD revisions, sample approvals, and production scheduling. A better approach is to choose a partner that offers rapid prototyping and keeps a rolling inventory of common lumber, plastic resins, or metal frames. That way, your custom spec is less about starting from scratch and more about configuring from proven building blocks—cutting lead time from weeks to days.
What really kills lead time isn't the manufacturing; it's the back-and-forth. Clear, upfront communication about your load requirements, handling environment, and budget lets a good supplier quote and build accurately the first time. Pair that with in-house cutting, assembly, and quality checks, and you can have a custom pallet spec delivered faster than many off-the-shelf options. No rushed air freight, no last-minute design changes—just a straightforward process that respects your schedule.
How to Spot a Supplier Who Treats AGV Compatibility as an Afterthought
Most vendors will nod along when you mention AGV integration, but the telltale sign comes when you ask for concrete proof. If they can't show you a documented interface spec, a list of tested robot models, or a live demo with an actual AGV navigating their equipment, you're likely dealing with a company that bolted on "compatibility" as a marketing bullet point. Watch how they respond to questions about handshake protocols, sensor placement, or load transfer timing. Vague reassurances like "we work with all major brands" without naming a single successful deployment should set off alarm bells.
Another red flag is a supplier who treats AGV compatibility as a future software update rather than a core design principle. If their engineering team needs to "look into" whether a particular AGV model can dock safely, or if they suggest you modify the robot's navigation to fit their machine, that's backwards. True compatibility means the equipment was designed with AGV pick-up points, clearance zones, and communication interfaces from the start. Ask for their CAD files and see if the AGV contact points are clearly marked, or if they look like an afterthought squeezed into available space.
Finally, check how they handle edge cases. A supplier who cares about AGV integration will have answers for uneven floors, battery swapping procedures, or what happens when the AGV loses connection mid-transfer. If they brush off these scenarios or claim they've never encountered them, it usually means they've never actually tested with a real fleet. Ask for a reference customer who runs AGVs daily—not a one-off pilot. If they can't provide one, you're better off looking elsewhere before the integration costs land on your plate.
The Real Cost of Cheap Pallets When Your AGV Fleet Runs 24/7
At first glance, saving a few dollars per pallet feels like an easy win—until the 3 a.m. call comes in. Automated guided vehicles don't forgive warped boards or loose fasteners the way a forklift operator might. A pallet with a slightly raised splinter can trip a sensor, force an emergency stop, and idle an entire charging line for twenty minutes while someone walks the floor to clear the fault.
Over a 24/7 operation, those minutes compound fast. Cheap wood also sheds debris that clogs casters and optical readers, which pushes maintenance crews into reactive mode instead of scheduled upkeep. The pallets themselves often fail after a handful of cycles, so you end up buying replacements more often—and paying freight on those replacements—while the machinery takes micro-hits that shorten component life.
The real expense isn't on the invoice. It's in lost throughput, extra labor hours, and the slow erosion of AGV reliability. Paying slightly more for consistent, automation-grade pallets usually returns that difference within weeks simply by keeping the fleet moving instead of nursing it through another shift.
FAQ
Start by requesting a dimensional stability report under full payload, not just a CAD drawing. The pallet's bottom deck clearance must stay within ±2 mm across the entire surface, or laser-guided AGVs will misread fork pockets. Ask for video of the pallet being picked up by an actual AGV, preferably at maximum load and after 100 automated cycles, because static measurements hide racking distortion.
Polypropylene and HDPE behave differently in a sealed container under tropical heat. HDPE creeps less under sustained load, but PP resists impact better during rough unloading. For export, specify a glass-filled PP if the pallet must handle AGV racking above 500 kg, and require a heat deflection temperature above 90°C. Avoid unmodified recycled resin, which can warp after one ocean voyage and cause pick-up failures at the destination warehouse.
Beyond ISO 8611 for pallet performance, ask for IPPC ISPM 15 compliance if any solid wood components are used, and UL 94 HB flame rating for plastic pallets entering North American DCs. For Europe, REACH and RoHS declarations are often contract requirements, not just paperwork. A supplier that cannot produce third-party load test reports for bottom deck deflection is not ready for automated cross-dock operations.
The biggest hidden issue is inconsistent pallet pocket height due to cooling shrinkage. If a mold is not compensated for shrinkage, the pocket opening can vary by 3–4 mm across one batch, which fools the AGV's laser profile scanner. Specify a tolerance of ±1 mm on fork entry height and ±0.5 mm on pocket width. Request a Go/No-Go gauge test report from the supplier, not just a sample measurement sheet.
Ask for cycle time data from their injection molding machines and their internal reject rate per cavity, not just total output. A supplier running multiple cavities with uneven cooling will produce pallets that pass visual checks but fail AGV pick-up after 48 hours of stacking. Insist on cavity-numbered samples from the middle and end of a production run, and compare their weight and pocket geometry against the approved golden sample.
Integral steel reinforcement bars in the fork entry area are a practical upgrade, but they must be fully encapsulated to avoid corrosion in sea air. Add anti-slip grommets or rubber inserts on the top deck only if the AGV uses a push-pull mechanism, otherwise omit them because they interfere with vacuum grippers. Four-way entry with chamfered lead-ins reduces docking errors by about 30% compared to two-way pallets in high-density racking.
Low-cost pallets often have flash or sharp edges from worn molds, which damage AGV sensors or conveyor belts. They also tend to use hollow ribbed decks that collapse under point loads from small AGV forks. Instead of chasing the lowest unit price, require a minimum top deck thickness of 5 mm in the fork contact zone and a 100% visual inspection certificate for flash removal. Paying 8–12% more per pallet typically eliminates a 20–30% rejection rate at the receiving dock.
Do not accept a single blanket lead time. Ask for stage-gated capacity reservation: 30% of the order produced in the first four weeks for the initial facility, with a mini-batch flight check. Then release the remaining volume only after the first container passes a 72-hour automated handling trial at your regional hub. This splits the risk and lets you catch mold drift before thousands of pallets are already on a vessel. Contractual penalties for dimensional non-conformance should be tied to the second batch, not the first.
Conclusion
Selecting an export-grade pallet supplier for AGV operations goes far beyond checking a dimension sheet. Even a few millimeters of sag or a slightly warped deck can throw off laser-guided navigation, turning a routine handoff into an unplanned line stop. The material spec matters just as much: plastic, wood composite, or steel must withstand repeated robotic clamping, high-cycle lifts, and uneven floor contact without cracking or shedding debris that gums up sensors. Global buyers frequently skip over phytosanitary certificates, ISPM-15 stamps, or regional fire and chemical compliance until a container gets held at the port—by then the cost is measured in stalled production, not just paperwork. The best suppliers treat AGV compatibility as an engineering requirement, not a marketing checkbox.
Custom pallet dimensions and reinforcement zones rarely have to mean months of waiting if the supplier keeps standard base molds and modular jigs on hand. Ask how they handle tolerance validation: do they run test loops with actual AGV models, or do they just send a CAD file and hope? Watch for red flags like vague answers on load deflection under robotic forks, no mention of edge radius for sensor clearance, or lead times that balloon when you request a non-standard size. Cheap pallets look attractive on a purchase order, but when your fleet runs around the clock, premature deck wear, cracked corners, and inconsistent fork entry points trigger repeated fault codes, extra maintenance shifts, and higher rejects. A supplier who truly understands AGV workflows saves money by reducing variability, not by shaving pennies off the pallet price.
Contact Us
Contact Person: Johnny
Email: [email protected]
Tel/WhatsApp: +86 18151010686
Website: https://lydstorage.com