Calcium Sulfate Six-Sided Steel-Faced Floor Solutions for Modern Construction Projects
2026-11-16
Ask any construction manager about raised access flooring and you'll hear two words: edge failure. That's the weak point in conventional calcium sulfate panels. Lipin Floor has a different answer—a six-sided steel-faced calcium sulfate floor that removes the weak point entirely. Designed for modern construction projects, it combines the stability of calcium sulfate with the toughness of steel on every face. In this post, we'll explore how that small change makes a big difference in load performance, fire safety, and installation speed.
Six Sides of Steel, Zero Compromises on Floor Performance
Six sides of steel form the backbone of this base, and every edge is machined to sit flat against hard floors without rocking, sliding, or leaving marks. The geometry isn’t just aesthetic—the hexagonal cross-section distributes weight evenly across all six contact points, so the chair stays planted when you lean, reach, or shift. That means no more mid-meeting wobble, no more rug snags, and no more wondering if the floor underneath is paying the price.
We treated floor contact as a performance spec, not an afterthought. The lower surface is finished with a low-friction polymer that glides over tile, hardwood, laminate, and low-pile carpet without scratching or squeaking. And because the steel is powder-coated rather than painted, it won’t chip, flake, or leave rust streaks when the seasons change or when a spilled drink goes unnoticed overnight.
The result is a base that feels heavy enough to anchor the chair yet moves with intention. You get the raw strength of six-sided steel and the finesse of a floor-safe glide, so you never have to choose between a stable seat and a clean floor.
The Hidden Strength of Calcium Sulfate in High-Rise Flooring
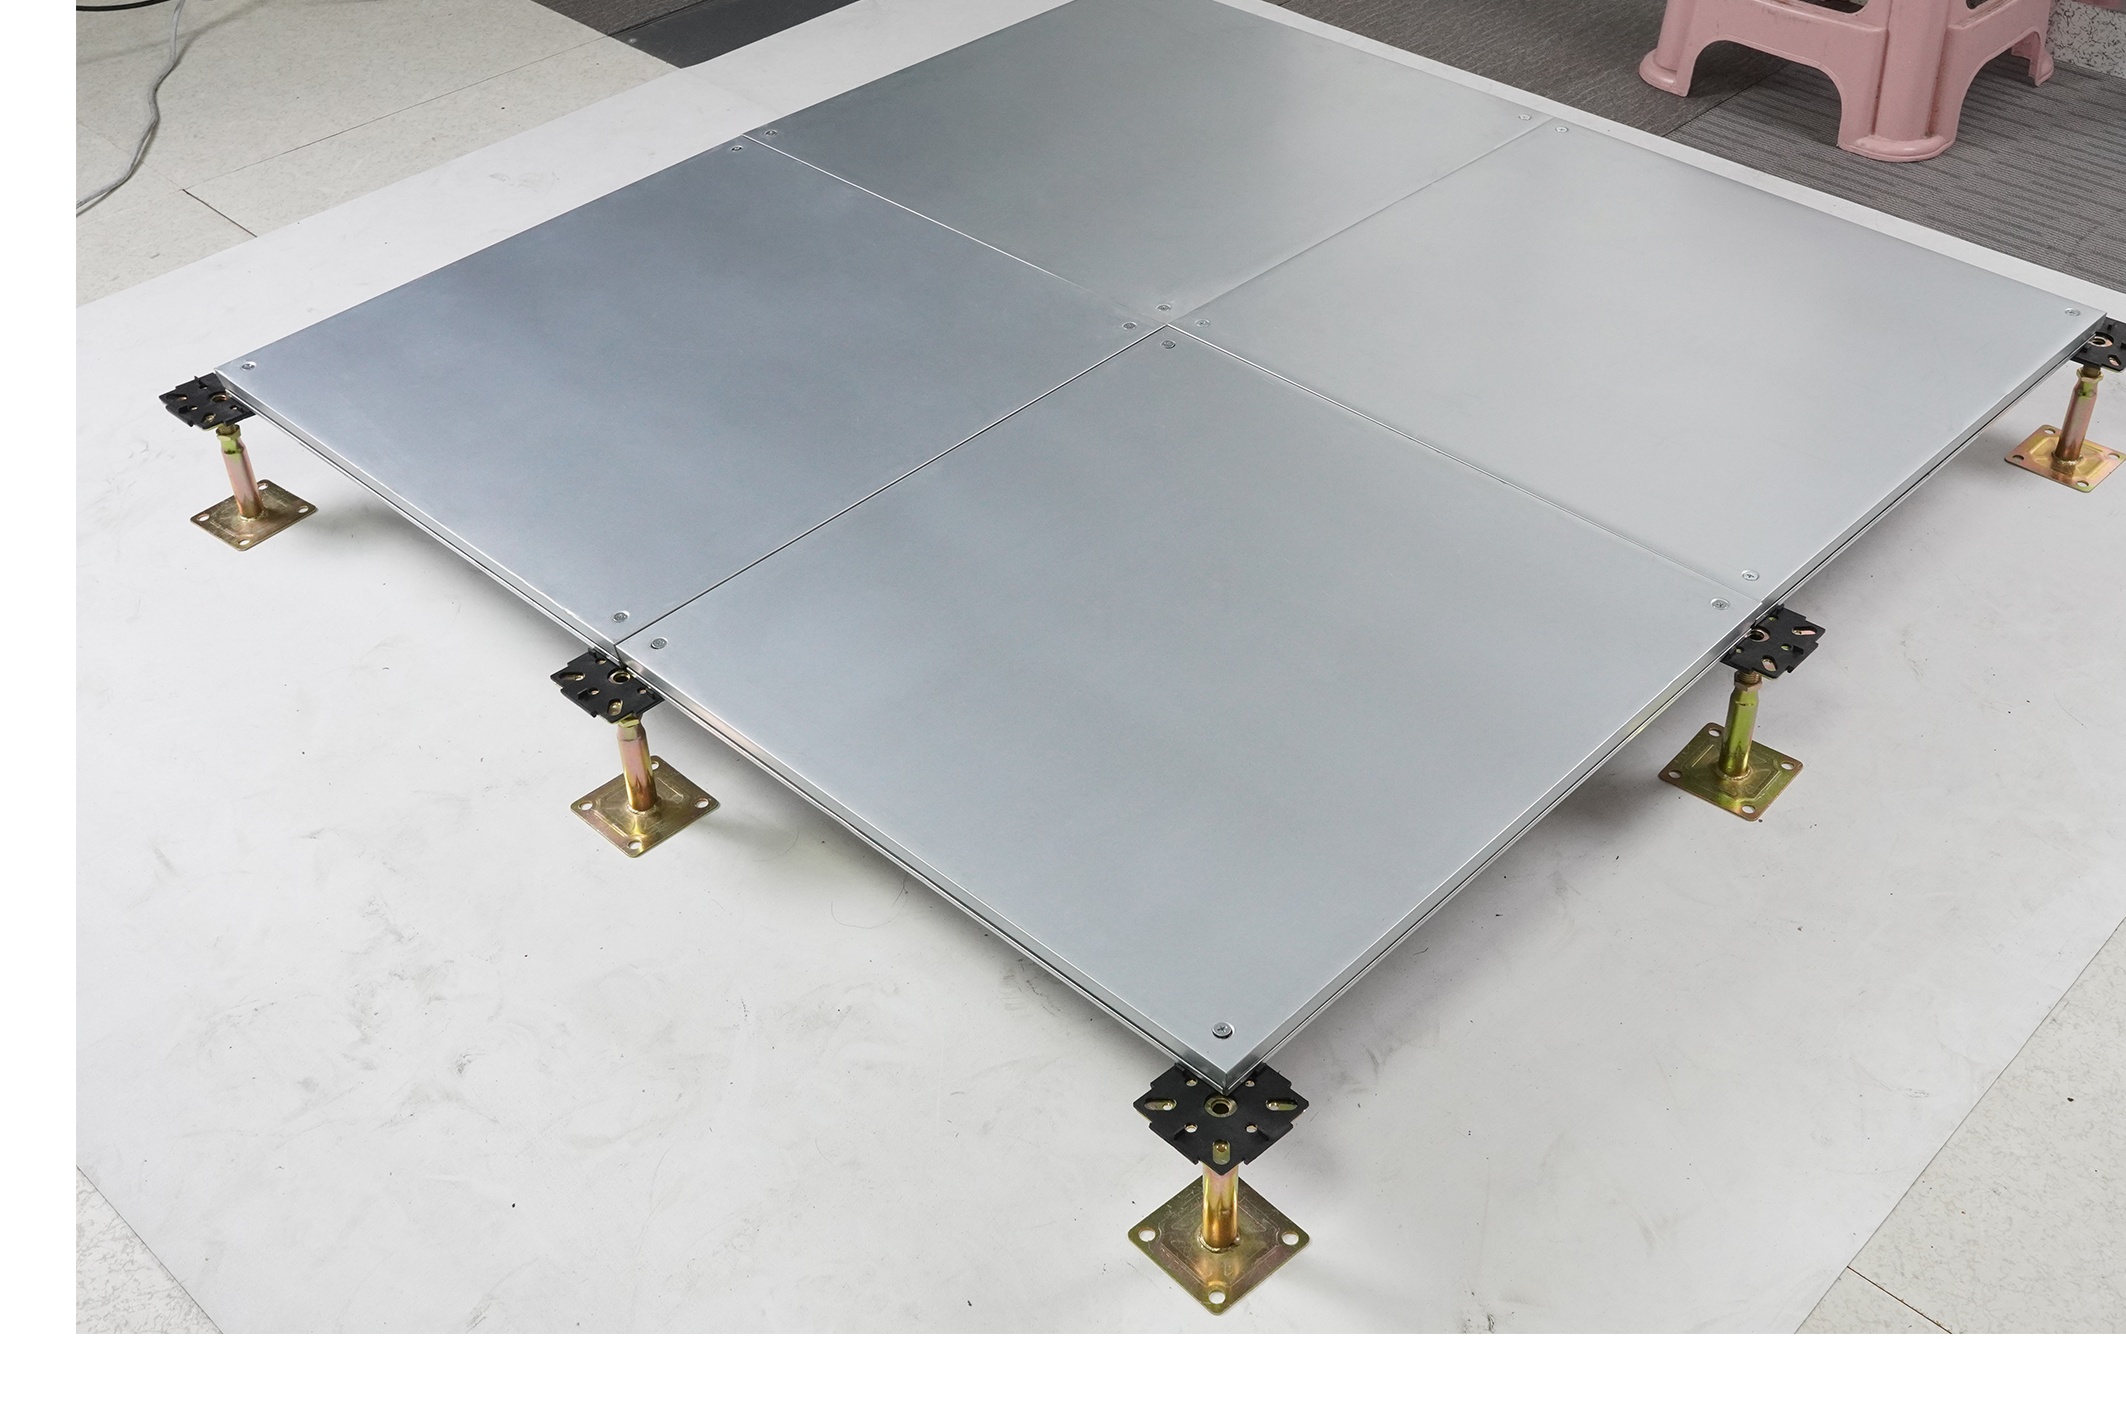
Calcium sulfate rarely gets the attention it deserves in high-rise flooring, yet its compressive strength quietly outperforms many conventional screeds. At a typical 25 mm thickness, a well-formulated anhydrite screed can reach 30–40 N/mm², which means less material is needed to carry the same load. That thinner section translates directly into lighter floors across dozens of storeys, easing the burden on the structural frame without sacrificing rigidity.
High-rise buildings also demand strict fire and acoustic separation between units. Calcium sulfate's crystalline structure holds chemically bound water, which is released slowly when exposed to heat, helping to slow temperature rise long before sprinklers activate. At the same time, its dense, low-porosity surface reduces airborne and impact sound transfer more effectively than sand-cement mixes of equal thickness, allowing floor build-ups to stay slim while still meeting code.
What really sets calcium sulfate apart in tower construction, though, is its dimensional stability. Because anhydrite screeds cure with minimal shrinkage and can be laid in large continuous bays, expansion joints become less frequent, and the risk of curling or cracking under heated floor systems drops significantly. Contractors can pour, pump, and finish these floors faster than traditional mortar beds, cutting both schedule time and long-term maintenance callbacks.
Cutting Weeks Off the Schedule with Modular Steel-Faced Panels
Modular steel-faced panels bring a quiet kind of speed to construction that traditional methods rarely match. Instead of waiting for on-site welding, curing, or weather-dependent masonry, crews can bolt pre-engineered panels directly into place. A single panel often spans floor-to-ceiling and wall-to-wall, which means fewer joints, fewer alignment checks, and far less time spent adjusting tolerances. On a recent mid-rise project, the switch from cast-in-place concrete to steel-faced modular panels cut the exterior enclosure schedule by nearly three weeks, even with the same crew size.
The real advantage shows up in how these panels let different trades overlap their work. While the steel-faced panels are being craned into position on one side of the building, interior framing or mechanical rough-in can proceed on the other, because the panels arrive with insulation, vapour barrier, and interior finish pre-attached. That eliminates the usual wait time between structural completion and weatherproofing. One superintendent described it as "getting the building dried-in before the roof is even fully tied off," which is exactly the kind of schedule compression you cannot fake with faster labour alone.
There is also a hidden time-saver in the way modular steel-faced panels handle design changes. Because the panels are fabricated off-site from shop drawings that are finalised before cutting begins, field modifications drop dramatically. When a window opening or a corner detail needs adjusting, the panel supplier can revise the next batch without stalling the whole line. That flexibility keeps the schedule from absorbing the typical slow-downs caused by RFI back-and-forth or rework. In the end, the weeks saved are not from doing the same work faster, but from removing the pauses, hand-offs, and corrections that usually pad a construction timeline.
Fire Ratings and Sound Control That Come Standard, Not as Add-Ons
Fire resistance and acoustic performance usually show up as optional upgrades that push budgets higher and complicate the build. These panels flip that approach. The standard product line already includes tested fire ratings and meaningful sound reduction, so you're not paying extra for baseline safety and comfort.
Since the fire and sound properties are part of the core panel construction, you don't need to add extra gypsum layers, insulation, or sealants just to meet common code requirements. That keeps wall profiles thinner, shortens installation time, and reduces the chance of on-site mistakes.
For anyone specifying or installing partitions, this standard approach means fewer trade-offs. The panels arrive ready to deliver both fire separation and acoustic control without special handling or custom detailing, making it simpler to achieve consistent results across an entire project.
Green Building Credits Start at Floor Level with Recyclable Panels
When architects chase green building certifications, they often overlook the most obvious surface underfoot. Recyclable floor panels made from reclaimed wood fibers, recycled aluminum, or bio-based resins can contribute directly to LEED and BREEAM credits, yet many project teams still default to conventional materials. The key is understanding how the panel's lifecycle—from raw material sourcing to end-of-life recovery—maps to specific credit categories like Materials & Resources or Waste Reduction. A floor isn't just a finish; it's a strategic asset that can nudge a project over the certification threshold.
The real advantage comes from panels designed for disassembly. Instead of glued-down systems that end up in landfill after a renovation, modern recyclable panels use mechanical locking or reversible adhesives, allowing them to be removed intact and either reused or sent back to the manufacturer. This closes the loop in a way that monolithic concrete or laminated vinyl cannot. Some manufacturers even offer take-back programs, which strengthens the chain-of-custody documentation required for credits. It's a quiet revolution—starting at floor level, but rippling through the entire supply chain.
Beyond the paperwork, there's a practical payoff. Recyclable panels often weigh less, install faster, and improve indoor air quality by avoiding urea-formaldehyde binders. For building owners, that translates into lower labor costs and healthier spaces, not just a plaque on the wall. As rating systems tighten their criteria around embodied carbon and circularity, floor panels are becoming one of the easiest ways to earn points without redesigning the whole structure. The next time a project team discusses green strategies, they might want to look down first.
From Server Rooms to Showrooms, One Flooring Approach Covers It All
Server rooms demand more than just a surface to walk on. They need flooring that handles static discharge, supports racks loaded with hundreds of kilograms, and allows precise airflow for cooling. The right approach here isn't a specialty product found only in data centers—it's the same modular system you'd see in a high-end car dealership. Each tile locks into place over a raised grid, creating a seamless path for cables and chilled air without sacrificing load-bearing strength. Technicians can roll heavy equipment across it daily, and if a tile ever gets damaged, replacement takes minutes, not hours.
Walk into a showroom and the requirements shift dramatically. Visitors notice color, texture, and how light bounces off the floor. Scratches from stiletto heels or dragged furniture are inevitable. This is where the same flooring approach earns its keep. The top layer can be finished in warm wood tones, polished concrete looks, or bold geometric patterns—all while maintaining a commercial-grade wear layer that resists scuffs and stains. Because it doesn't rely on adhesives or permanent installation, showroom layouts can change seasonally without tearing up the subfloor. A new car launch, a fashion week display, or a tech product reveal all happen on the same foundation.
What makes this flooring approach truly work across such different spaces is its refusal to force a trade-off. Server rooms get the anti-static and load-bearing performance they need. Showrooms get design freedom and durability. Facility managers get a single system to stock, clean, and repair. Instead of maintaining separate flooring inventories for back-of-house and front-of-house, teams standardize on one platform—reducing training time, spare parts waste, and renovation costs. The next time you walk from a humming data hall into a polished retail floor, look down. You might be standing on the same engineered surface.
FAQ
It comes down to dimensional stability and fire performance. The core won't warp or swell with moisture changes, and it gives a much cleaner fire rating without needing extra treatments.
Each panel has steel bonded to all six faces, so edges and undersides get the same protection as the top. That helps prevent corner damage during transport and provides a continuous tough surface on site.
Yes, the weight-to-strength ratio makes them easy to handle off-site and assemble quickly, and the consistent dimensions help keep modular joints tight.
The surface is flat and stiff enough for most finishes, including tile, stone, engineered wood, and vinyl. You still need the usual primers or underlayment for specific adhesives, but no extra leveling is needed.
Calcium sulfate is non-combustible and the steel skin adds a barrier, so floors built with these panels can meet high fire-resistance ratings without additional board layers.
The core doesn't absorb water like wood or gypsum board, and the steel facing keeps most moisture out. Joints should be sealed, but brief exposure to rain won't ruin the panel.
Hardly any. Sweep or mop as usual, keep the joints sealed, and replace a damaged section if necessary—most panels can be swapped without tearing out the whole floor.
The dense core cuts down both airborne and impact sound transmission, so you get a quieter floor without adding thick underlayments.
Conclusion
For high-rise projects where floor performance cannot be left to chance, the calcium sulfate six-sided steel-faced system delivers a rare combination of rigidity and control. The steel enclosure on all six faces locks in a dense sulfate core, creating panels that handle heavy point loads and rolling traffic without flexing or cracking. Because they arrive as modular units, installation crews can set large areas in a fraction of the time wet trades demand—saving weeks on the schedule instead of days. Fire resistance and acoustic separation are built into the panel itself, not added later with extra layers or coatings, so the floor assembly stays thinner while meeting strict code requirements.
What sets this approach apart is how it behaves across radically different environments. The same panel system that supports a server room’s underfloor cabling and cooling airflow also works as a polished finished surface in a retail showroom, with no change in detailing or subfloor prep. At end of life, the steel and calcium sulfate core can be separated and recycled, which helps projects earn green building credits without chasing exotic materials. By covering structural, acoustic, thermal, and finish needs in one pre-engineered floor, the solution removes a lot of coordination risk that typically falls on the construction team.
Contact Us
Contact Person: yuki
Email: [email protected]
Tel/WhatsApp: +86 18664390732
Website: https://www.lipinfloor.com/