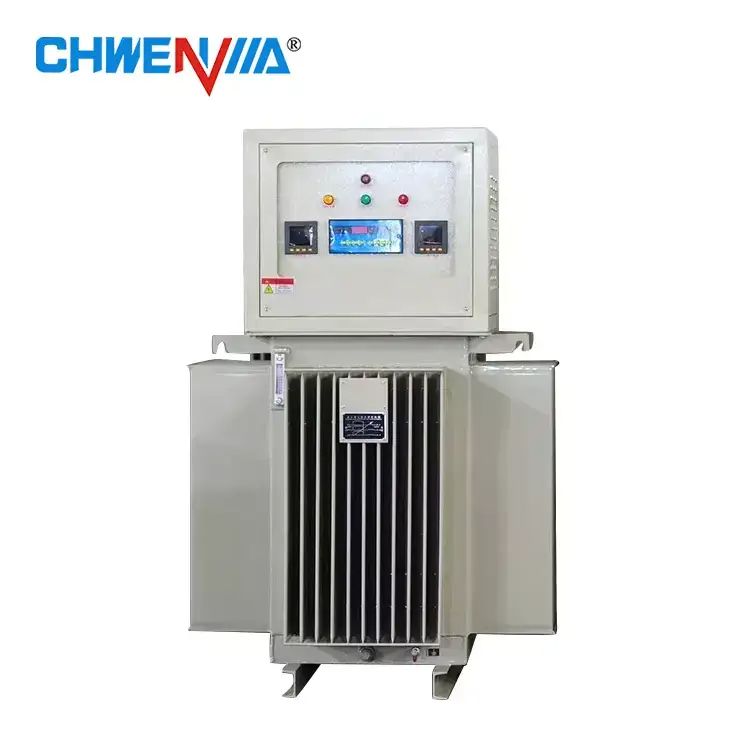
Best Oil Immersed Voltage Stabilizer Factory Qualities That Ensure Stable Power
2026-09-12
In an era where voltage fluctuations can silently degrade equipment and halt operations, choosing the right oil immersed voltage stabilizer manufacturer is not a mere procurement decision—it is a safeguard for your entire power infrastructure. While many factories claim reliability, only those with rigorous material selection, precision winding, and full-load testing can deliver the stability your critical loads demand. As you explore the essential qualities that set top-tier suppliers apart, one name consistently stands out: Wenma. Known for its engineering depth and transparent production practices, Wenma challenges the industry standard by turning every stabilizer into a long-term asset. But what exactly should you look for in a factory? Read on to uncover the traits that separate genuine stability from superficial promises.
Winding Precision That Keeps Output Flat When Input Swings
Every turn of wire in these magnetics is placed with deliberate tension and alignment, so the leakage inductance and parasitic capacitance stay within a very narrow band. That means the converter doesn't fight its own stray elements when the line voltage dips or spikes. Instead of a mushy response to input changes, the output holds its shape because the winding geometry itself refuses to introduce noise or time constants that would otherwise ripple through.
A tightly wound coil also keeps the primary and secondary coupling uniform across the entire window. When the input swings quickly, uneven coupling would normally create hot spots of flux imbalance, pushing the output voltage up or down before the feedback loop can react. Here, the precision layering and interleaving of windings make each switching cycle see nearly the same electromagnetic environment, so the output stays flat even during fast transients.
This isn't just about machine repeatability. The winding process uses controlled layer transitions, minimal overlap, and consistent spacing to reduce proximity effect losses that would otherwise vary with input voltage. Those losses, if left unchecked, act like a hidden load that changes with operating point. By keeping them constant, the output regulation gets one less variable to correct for, and the flatness you see on the bench is already built into the copper.
Tank Sealing Methods That Block Moisture Before It Reaches the Oil
Moisture is the silent killer of stored oil, and the first line of defense sits at the tank's sealing points. Traditional gaskets and O-rings degrade unevenly under temperature swings, creating microscopic channels that let humid air creep inward. A more reliable approach involves compression seals made from fluorosilicone or hydrogenated nitrile—materials that keep their elasticity far longer than standard rubber. These aren't just slapped on; they're paired with precisely machined flange faces to eliminate low spots where condensation can pool. The result is a barrier that stays intact even when the tank breathes during fill and drain cycles.
Beyond static seals, some tanks now use a dynamic moisture barrier in the vent system. Instead of a simple filter, a desiccant breather traps water vapor before it can enter the airspace above the oil. The clever part is the regeneration cycle: as the tank exhales, dry air from inside pushes back through the desiccant, purging a portion of the captured moisture. This means the system doesn't just block humidity—it actively pumps it back out. For tanks in coastal or high-humidity areas, combining this with a spring-loaded pressure relief valve keeps the internal atmosphere slightly positive, so outside air never gets a chance to seep in through imperfections.
The most overlooked sealing point is often the access hatch or manway cover. Even a brand-new tank can leak moisture here if the cover is torqued unevenly or the gasket sits in a groove that holds water after rain. A practical fix is to switch to a double-lip seal with a weep hole between the lips. Any moisture that gets past the outer lip drains away through the weep hole instead of being pushed inward by temperature cycles. Paired with a simple routine—checking the torque pattern every few months and replacing gaskets at the first sign of surface cracking—this method keeps oil dry without expensive retrofits. Dry oil means fewer acids, less sludge, and a longer life for both the lubricant and the machine it protects.
Load Bank Testing Beyond the Nameplate Rating
Most operators stop at the nameplate rating, but a load bank can push far past that static number. The idea isn’t to simply confirm what the generator can do on paper—it’s to reveal how the machine behaves under stress that no spec sheet will ever show. By gradually increasing the applied load beyond the listed kW or kVA, you expose weak points in fuel delivery, cooling efficiency, and voltage regulation that would stay hidden during normal operation.
Pushing beyond the nameplate isn’t about reckless overload. It’s a controlled test that often uncovers latent issues like clogged injectors, failing thermostats, or deteriorating insulation. A generator might hold its rated load for hours, then stumble when asked for an extra ten percent during a hot afternoon. That stumble is exactly what you want to find before the grid fails, not after.
The real value emerges when you monitor exhaust temperatures, pressure drops, and transient response at elevated loads. These readings tell you whether the unit still has usable headroom or if it’s already running on the edge. Many older machines carry a nameplate number that assumes ideal conditions—cool intake air, clean filters, fresh oil. Testing beyond that number forces the generator to prove itself under real-world degradation, which is far more useful than a factory certificate.
Core Steel Sourcing That Starts With Grain Orientation Checks
Sourcing core steel without verifying grain orientation is like buying a compass without checking if the needle moves. The magnetic performance of every transformer, inductor, or motor depends on how well the steel's crystal structure aligns along the rolling direction. Before we commit to any supplier, our engineers pull samples from the incoming coil and run Epstein frame tests to measure core loss and permeability at different flux densities. Only material that shows a sharp Goss texture—where most grains sit within a few degrees of the ideal orientation—makes it past the first gate.
That early check does more than filter out subpar lots; it shapes the entire sourcing conversation. We ask mills for their orientation distribution data, not just the typical thickness and coating specs. Some suppliers claim high-grade silicon steel, but their grain scatter tells a different story under a microscope. By insisting on orientation data before pricing discussions, we avoid the trap of buying on chemistry alone. This approach has repeatedly saved us from coils that would pass a standard chemistry check but fail under real AC magnetization.
What starts as a grain orientation check becomes a supplier qualification tool. Mills that can consistently hit tight orientation tolerances tend to have better rolling and annealing control, which means fewer hidden defects further down the line. In our experience, the best core steel relationships are built with partners who welcome this scrutiny—they know their process, and they know that a buyer who asks about Goss texture is a buyer who understands what makes a core perform.
Continuous Oil Filtration Instead of One-Time Factory Fills
The idea that oil only needs to be clean when it leaves the factory ignores what happens inside a running machine. Particles from wear, dust ingress, and thermal breakdown steadily contaminate the fluid long before the next scheduled change. Continuous oil filtration attacks this problem at the source, circulating the oil through fine media or centrifugal separators around the clock so that contaminants never get a chance to settle or cause damage.
In hydraulic and lubrication systems, even particles smaller than the clearance between moving parts can create abrasive wear over time. A bypass filter loop operating continuously can hold ISO cleanliness levels far tighter than a one-time fill ever could. This keeps valves from sticking, reduces heat generation, and preserves additive packages that would otherwise be depleted by oxidation. The result is not just cleaner oil, but a more predictable and longer-lived system.
Shifting from periodic factory fills to continuous filtration does require an upfront investment in hardware and plumbing. However, many plants find the payback comes quickly through extended oil life, fewer disposal events, and far less unplanned downtime. Instead of treating oil as a consumable to be replaced on a fixed schedule, the system treats it as an asset to be maintained in service, which changes both maintenance routines and operating costs for the better.
Real-Time Thermal Mapping During Final Run-Ins
During final run-ins, the break-in process often reveals friction points that only appear under gradual load increases. Instead of relying on periodic spot checks with a handheld probe, real-time thermal mapping uses an array of infrared sensors or a mounted thermal camera to watch the entire assembly warm up together. The data streams continuously, so a bearing cap that climbs five degrees faster than its neighbour becomes visible before it turns into scoring or a seized shaft.
Operators set upper and differential limits tied to each stage of the run-in cycle. When a gear mesh or seal begins to heat unevenly, the map shows the gradient shifting rather than just a single number on a gauge. That early pattern matters because it points to alignment drift, insufficient lubrication, or a tight clearance that would otherwise hide until the final load step.
The payoff shows up in shorter run-in windows and fewer post-commissioning teardowns. A complete thermal record also gives the maintenance team a baseline for the machine's first weeks in service, so later deviations are easier to judge without guesswork.
FAQ
Look beyond glossy brochures. A dependable factory will have a vacuum impregnation line for the windings, use high-grade silicon steel for the core, and run full-load temperature rise tests on each unit—not just a random sample. Ask to see their oil purification setup and verify that every stabilizer gets a dielectric strength check before shipping.
The oil does two jobs: it carries heat away from the windings and it prevents arcing. Poor-quality or contaminated oil breaks down under heat, creating hot spots that can shift resistance and cause voltage drift. Factories that filter and test the oil before filling give you a stabilizer that holds steady even when ambient temperatures climb.
It usually comes down to magnetic circuit design and winding geometry. Factories that cut steel cheaply or wind coils unevenly end up with higher leakage reactance, so the output sags the moment a motor starts. The good ones test each unit with simulated load swings—switching on inductive and resistive banks—before it leaves the floor.
Vacuum drying of the core and coils before oil filling, proper varnish impregnation, and careful welding of the tank are non-negotiable. Cheap units often skip the vacuum step, leaving moisture inside that breaks down the oil over time. A reliable factory will also anneal the core laminations to restore magnetic properties after cutting.
Insist on seeing the test bay, not a certificate. A meaningful test includes running the unit at 110% load for several hours, checking winding temperature rise, testing insulation resistance before and after heat soak, and taking an oil sample for moisture and acidity. Those results tell you how the stabilizer will behave after years of thermal cycling.
Absolutely. High-permeability grain-oriented silicon steel reduces core losses and keeps the magnetic flux stable under varying input voltage. Oxygen-free copper windings with tight, uniform layering avoid localized hot spots. Cheaper materials may pass a bench test, but they drift once the unit is installed in a hot, dusty environment and asked to hold voltage within a tight band.
Beware of factories that won't let you see the assembly floor. Other warning signs: no real-time temperature rise monitoring during load tests, oil that arrives in unmarked drums, missing data on core lamination thickness, and welds that look uneven or painted over. If they cannot provide a serial-numbered test report for the exact unit you are buying, walk away.
Ask both to send a unit to an independent lab for a 72-hour endurance test, or better yet, visit in person and watch them build and test your order. Request oil analysis records from the last six months and speak to a customer who has had the unit running under heavy load for at least two years. The factory that gives you transparent, verifiable data instead of marketing phrases is the one to trust.
Conclusion
The best oil immersed voltage stabilizer factories treat output flatness as a mechanical discipline, not a marketing promise. Their winding teams measure coil geometry after every layer, tightening tolerance windows so voltage correction happens without overshoot or hunting when the grid sags or spikes. That same obsession carries into tank assembly: gasket channels are machined flat, bolts torqued in sequence, and every weld is vacuum-box tested before oil ever enters. Moisture doesn't get a chance because sealing is treated as a pressure boundary, not a simple lid. Core steel arrives with mill certificates, but incoming inspectors still run Epstein frame tests and check grain orientation under polarized light before a single lamination is cut. For them, core loss isn't a catalog number—it's a thermal and acoustic fingerprint they have to verify.
Once assembled, these stabilizers are pushed past nameplate conditions. Load bank testing includes step changes, unbalanced phases, and sustained overloads that expose weak terminations or hot joints a standard factory run-in misses. Oil is not just filled once and forgotten. Continuous filtration loops pull moisture and particulates out while the unit cycles, keeping dielectric strength high from the first energization to final delivery. During the last run-in, thermal cameras map winding and bushing temperatures at full load, and the data is compared against predicted hotspots. If a deviation shows up, the unit is pulled and corrected, not shipped with a note. That combination—verification beyond the label, sealing as a system, and real thermal evidence—makes certain factories stand out for stable power delivery.
Contact Us
Contact Person: Mr. Jiang
Email: [email protected]
Tel/WhatsApp: +86-15057775503
Website: https://www.avrfactory.com/